China Top 10 Visual Inspection Device Manufacturers
China’s visual inspection market has grown alongside electronics, automotive, pharmaceutical, and food production. A Visual Inspection Device can check tiny solder joints, bottle seals, printed codes, or surface scratches at production speed. Yet a camera alone does not guarantee reliable results. Lighting, lens selection, image-processing software, conveyor stability, and operator training all shape inspection quality.
Quality-management expert W. Edwards Deming offered a useful caution: “Inspection is too late. The quality, good or bad, is already in the product.” His point still matters. Automated inspection can detect defects and support process improvement, but it cannot replace sound production controls. This overview of China’s top 10 Visual Inspection Device manufacturers is a practical starting point, not a universal ranking. Company strengths vary by application, factory scale, integration needs, and service coverage. Buyers should examine sample images, false-reject rates, inspection speed, calibration routines, software usability, and technical support. Ask how systems perform under changing light, dust, vibration, or product variation. Small details count.
A polished demonstration may not reflect a demanding production line. Not every specification tells the whole story. Supplier claims should be checked through trials, customer references, and clear acceptance criteria. The right choice depends on the defect, the production line, and the cost of missed or rejected products.
Definition and Core Functions of Visual Inspection Devices
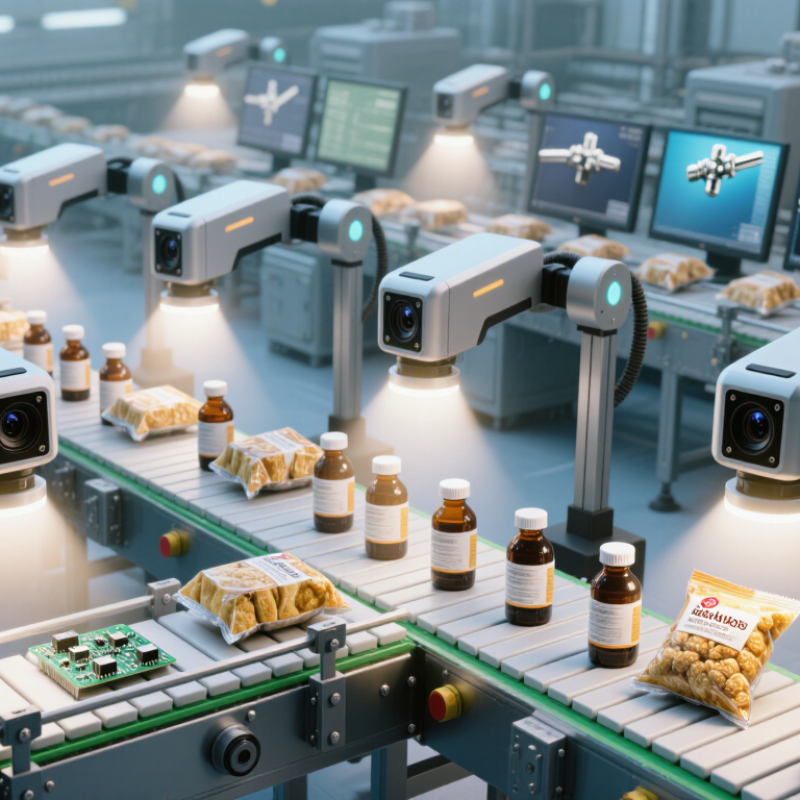
A visual inspection device is an imaging system that captures product or process details and checks them against defined criteria. A typical setup combines a camera, lens, controlled lighting, and image-processing software. It may detect surface defects, measure dimensions, verify component presence, or read printed characters. On a production line, it could flag a chipped edge or a misaligned cap within seconds.
Lighting matters.
The system’s core function is not simply taking a clear picture. It must turn image data into a repeatable decision, such as pass, reject, or review. Some systems use rule-based measurements; others apply machine-learning models to recognize more varied defects. The result depends on image quality, inspection settings, and representative training examples.
Not magic.
Unusual materials or changing reflections can still produce missed defects or false alarms, so human review and regular checks remain important.
MarketsandMarkets’ Machine Vision Market report estimated the global market at USD 12.1 billion in 2023 and projected USD 17.2 billion by 2028. That figure covers a broader market than inspection devices alone, but it signals growing industrial use of image-based automation. It is market context, not proof that every installation improves quality.
A careful evaluation should compare inspection results with independently checked samples and document the conditions under which the system performs well.
Major Technologies Used in Visual Inspection Systems
Major Technologies Used in Visual Inspection Systems
Visual inspection systems turn physical defects into measurable image data. Their core components are cameras, lenses, lighting, and processing software. Area-scan cameras capture full images; line-scan cameras build images as products move past. Global-shutter sensors reduce motion blur on fast conveyor belts. Light matters. Diffuse lighting reveals dents, while coaxial lighting can expose scratches on flat surfaces. A poorly chosen light can hide the defect entirely.
Two-dimensional imaging suits label checks, missing parts, and surface marks. For height and shape, systems use 3D methods such as structured light or laser triangulation. Deep-learning models can classify irregular defects, while rule-based vision remains useful for stable measurements. Neither approach fixes poor image capture. A glossy cap can fool a model; that practical limitation deserves testing under real production conditions. Multispectral imaging can distinguish materials that look similar under ordinary light, though it adds cost and setup complexity.
MarketsandMarkets’ 2023 Machine Vision Market report estimated a market value of $12.1 billion in 2023 and forecast $19.6 billion by 2028. This is a market forecast, not a guarantee of inspection accuracy. In practical installations, edge processors can reduce delays by analyzing images near the production line. Still, each product, camera angle, and lighting setup may need its own validation. The overlooked detail is often simple: dust on a lens can change results.
Criteria for Evaluating Chinese Manufacturers
When evaluating Chinese visual inspection device manufacturers, begin with the production task, not a catalogue image. Specify the material, surface finish, defect size, line speed, and available installation space. A glossy metal part may need different lighting from a matte plastic component. Ask the supplier to inspect your actual samples under realistic conditions. Numbers matter. Request results for missed defects and false rejects, not just a headline accuracy figure. No test covers every production variation, so agree on how performance will be checked after installation.
Review the engineering and support behind the machine. Ask who develops the imaging and inspection software, how lighting and camera settings are controlled, and whether inspection records can be exported. Request a repeatability test, a sample validation report, and clear acceptance criteria before purchase. Check the proposed integration with your conveyor, control system, and factory network. Also confirm training, spare-part availability, and response times for technical support. Test it live. A polished demonstration can still differ from day-to-day production; that gap deserves careful discussion.
Tips: Bring varied samples, including borderline defects. Real samples help. Record the test conditions and keep the results. If a supplier cannot explain a limitation clearly, pause and ask for another trial. I would not treat one successful demonstration as proof of long-term reliability.
China Top 10 Visual Inspection Device Manufacturers
Suggested Criteria for Evaluating Manufacturers
Suggested evaluation weights (total: 100%), not measured company ratings. Assess optical performance, inspection speed, repeatability, adaptability, integration, service, and documentation against your application requirements.
Profiles of Ten Leading Visual Inspection Device Manufacturers in China
Profiles of ten leading visual inspection device manufacturers in China reveal a market shaped by varied production needs. Some firms focus on compact cameras and lighting for electronics lines. Others build integrated systems for checking packaging, machined parts, or printed surfaces. Their differences matter. A device designed for a fast conveyor may not suit a small workshop with frequent product changes.
A useful profile looks beyond product descriptions. It considers camera resolution, lens options, inspection speed, and how clearly results appear on the operator’s screen. For example, a line checking tiny scratches may need stable lighting and careful image setup, not simply a higher-resolution camera. Support also deserves attention: installation guidance, sample testing, and access to replacement parts can affect daily use. Details matter.
Manufacturer claims are best treated as starting points. Ask for trial results using representative parts, including difficult samples with glare, dust, or subtle defects. Compare how each system handles false alarms and missed defects, and check whether operators can adjust settings without lengthy retraining. Published specifications rarely show every factory condition. That is an imperfect way to judge equipment, but real production trials can reveal gaps that brochures miss. A sound profile should therefore describe capabilities, limits, and the applications each manufacturer serves, rather than relying on broad claims of superiority.
Industries Served and Emerging Market Trends
Visual inspection devices serve very different production environments. In food processing, cameras check seal integrity, label placement, and uneven fill levels. A small crease on a pouch can matter. In pharmaceutical packaging, inspection systems look for missing tablets, damaged cartons, and unclear printed codes. These checks support consistent quality, but they do not replace trained staff or documented procedures.
Electronics manufacturers use high-resolution imaging to find soldering defects and misplaced components. Automotive plants inspect welds, surface finishes, and part dimensions, often while products move along fast lines. Textile and glass producers also rely on vision tools to spot flaws that are difficult to see under ordinary lighting. The right setup depends on the material, speed, and acceptable defect range. One camera rarely fits every task.
Market trends are moving toward AI-based analysis, 3D imaging, and easier connections with factory data systems. Edge processing can shorten response times by evaluating images near the production line. Better lighting and simpler operator screens matter just as much. Useful details are often mundane. Emerging systems still need careful testing with real defects, changing shifts, and dusty lenses. Automation is not magic. Some detection models miss unusual flaws, and upgrades can add complexity. Manufacturers should compare false alarms, inspection speed, and maintenance needs before choosing equipment. The smartest system is one workers can verify and keep running.