How to Choose the Best Optical Sorting System?
Choosing the right Optical Sorting Systems solution begins with the material, not the machine brochure. A line sorting mixed produce may need to detect bruises and foreign material, while a recycling plant may focus on resin type, color, or particle size. The right choice depends on what must be removed, the required throughput, and the quality standard for the final product. Small details matter: belt speed, lighting, dust, washdown routines, and the space available for maintenance.
Before comparing models, ask suppliers to run representative samples under realistic conditions. Request measured results for detection accuracy, usable throughput, false rejects, and product loss. Check how quickly operators can adjust recipes and how local service teams handle faults. A demonstration with clean sample material can look impressive. Your own feedstock may behave differently. That deserves a hard look.
I can’t responsibly provide a named expert’s quotation without a verifiable source. For a reliable introduction, share an article or expert reference, and the quotation can be included with accurate attribution.
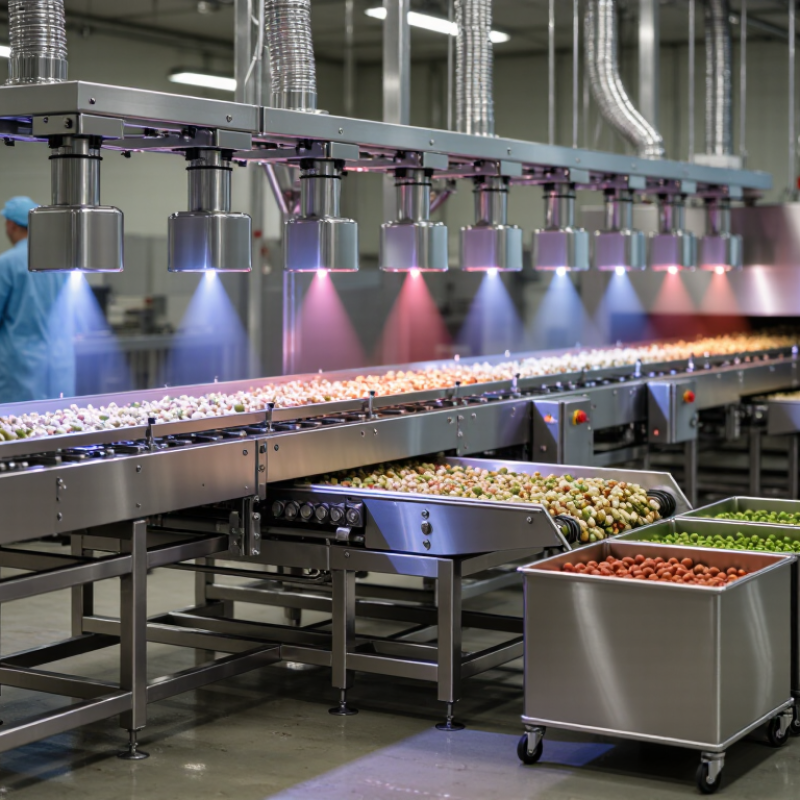
Table of Contents [Hide]
Define Your Sorting Goals and Performance Requirements
Before comparing optical sorting systems, define the material you need to separate and the outcome that matters most. Is the priority higher product purity, better recovery, or fewer manual inspection hours? Set a baseline using representative samples, including mixed sizes, surface moisture, and seasonal variation. Measure real samples.
For food operations, the scale of loss makes precise targets important. FAO’s 2019 State of Food and Agriculture estimated that about 14% of food is lost between harvest and retail. UNEP’s Food Waste Index Report 2024 estimated 1.05 billion tonnes of food waste in 2022. These figures describe different stages, not sorting performance. They show why plants should track usable yield and rejected material separately.
Specify throughput in tonnes per hour, acceptable defect levels, recovery rate, and false-reject limits. Test the system at normal speed, not only with carefully prepared samples. Record results by product type and operating condition. Ask how frequently settings need adjustment, and who will verify performance after installation. A clean test lot can hide a difficult feed stream. I would be wary of a single headline accuracy number; it may not reflect your line. Then test again. Make sure the acceptance criteria reflect actual production, including brief stoppages and changing input quality.
How to Choose the Best Optical Sorting System? - Define Your Sorting Goals and Performance Requirements
| Sorting Goal | Performance Requirement to Define | How to Measure It | Example Starting Point |
|---|---|---|---|
| Remove unwanted material | Specify the contaminants to reject, including their appearance, size, and frequency in the feed. | Count or weigh contaminants in representative feed and sorted-product samples. | List each reject category separately, such as discolored pieces, foreign materials, or off-spec products. |
| Meet product-purity requirements | Set the maximum acceptable amount of unwanted material in the accepted product. | Measure the composition of samples collected from the accepted-product stream. | Set a trial target based on the product specification and customer requirements; confirm it with testing on actual material. |
| Protect recovery of saleable product | Define how much acceptable material may be lost with the reject stream. | Compare the mass or count of acceptable material in the input and reject samples. | Establish a recovery target alongside the purity target, since increasing rejection can also increase good-product loss. |
| Achieve the required line capacity | Specify the required feed rate and the expected operating conditions, including feed consistency. | Record sustained throughput during a production-representative trial, not only a short peak run. | Use the required production rate as the minimum design basis and test with the expected material mix and feed presentation. |
| Sort within a defined particle-size range | State the minimum and maximum dimensions of material to be sorted, including expected size variation. | Measure representative particles and check sorting performance across the size range. | Document the size distribution of the real feed; confirm that the proposed machine configuration supports it. |
| Detect visually distinguishable defects | Identify the color, shape, surface, or other detectable differences between accepted and rejected material. | Test representative examples of each defect under the intended lighting, belt speed, and material orientation. | Provide samples that include normal variation, borderline cases, and the least-visible defects. |
| Maintain stable operation | Define the operating hours, cleaning intervals, changeovers, and acceptable downtime for the application. | Track availability, stoppages, cleaning time, and performance over a representative production period. | Include routine cleaning and planned maintenance when estimating usable production time. |
| Integrate with the existing process | Specify available floor space, conveyor interfaces, utilities, material flow, and reject handling. | Review the line layout and confirm that accepted and rejected streams can be collected without disrupting production. | Document upstream and downstream equipment, installation constraints, and required control-system connections. |
| Verify performance before purchase | Agree on test materials, sampling methods, operating conditions, and acceptance criteria. | Run a controlled trial using representative feed and independently check the resulting product and reject streams. | Evaluate purity, recovery, throughput, and operating stability together rather than relying on a single metric. |
Note: Performance targets depend on the material, defect characteristics, feed presentation, and operating conditions. Treat the examples as planning guidance and confirm final requirements through representative testing.